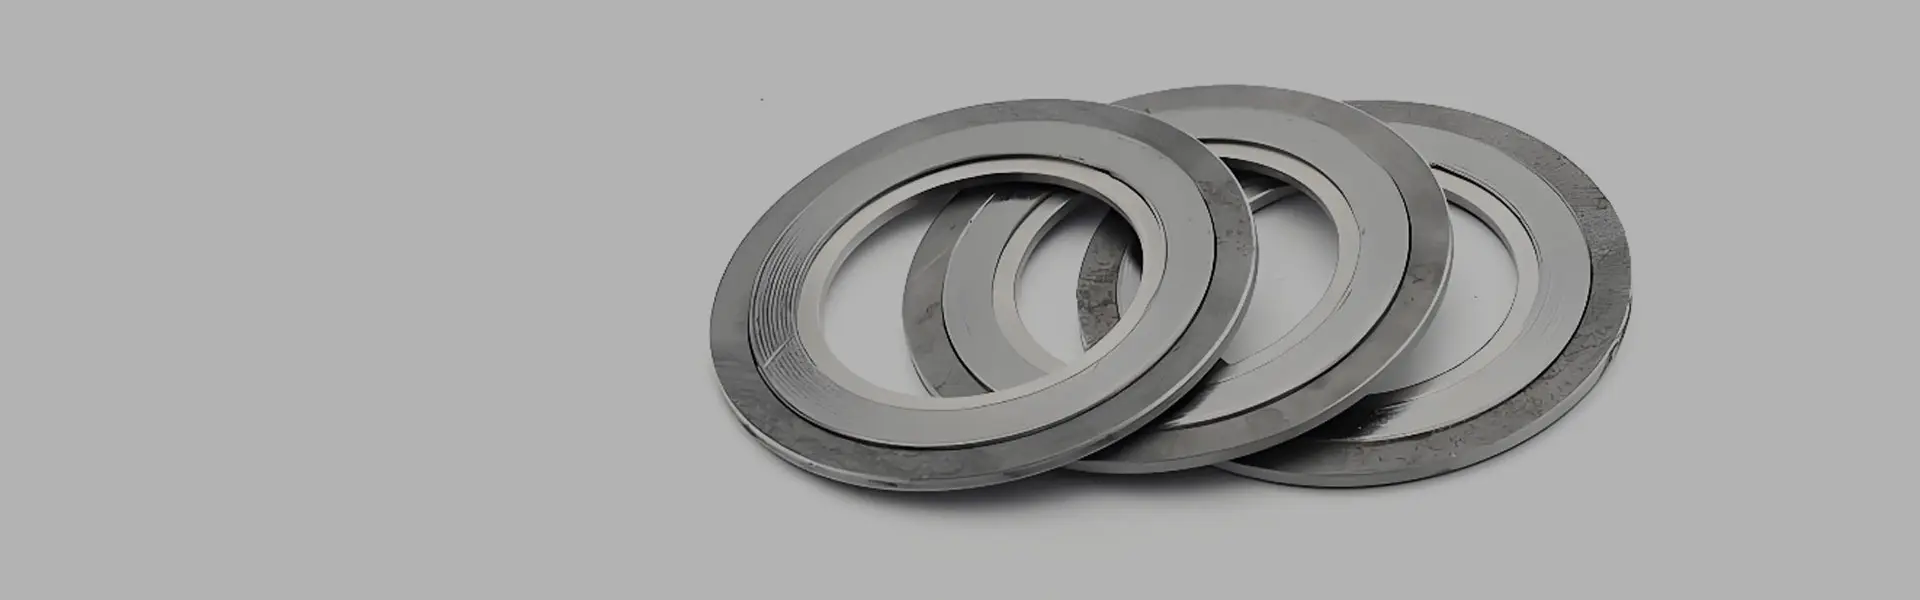
How do you properly install and tighten a spiral wound gasket? This seemingly simple question is critical for procurement professionals who understand that a flawless installation is the only guarantee of a leak-free, safe, and long-lasting seal in demanding industrial applications. A single misstep during installation can turn a premium gasket into a costly failure point. This guide cuts through the complexity, offering a clear, actionable roadmap. We'll explore common installation pitfalls, provide step-by-step solutions, and show how partnering with a specialist like Ningbo Kaxite Sealing Materials Co., Ltd. ensures you not only buy the right gasket but also secure its optimal performance from the very first bolt tightened.
Article Outline:
Imagine a high-pressure steam line scheduled for a routine shutdown. The maintenance team, pressed for time, installs a new spiral wound gasket. They skip cleaning the flange faces, use an old bolt pattern, and torque the bolts unevenly with an uncalibrated wrench. Upon startup, a persistent, dangerous leak appears, forcing an unplanned, expensive shutdown. This scenario is avoidable. The core problem isn't the gasket, but the installation protocol. Proper installation begins long before the gasket is unpacked. It requires meticulous surface preparation, correct gasket centering, and an understanding that the gasket is a precision component, not a consumable filler. A gasket from a trusted manufacturer like Ningbo Kaxite Sealing Materials Co., Ltd. is engineered for performance, but its potential is only unlocked with correct handling.

Key parameters to verify before installation:
| Pre-Installation Check | Specification / Action | Consequence of Neglect |
|---|---|---|
| Flange Surface Condition | Clean, undamaged, with proper serration (ASME B16.5) | Inadequate sealing, gasket blow-out |
| Gasket Dimensions (ID/OD) | Match flange standards exactly; ensure proper centering | Internal or external leakage paths |
| Bolt/Nut Condition | Clean, lubricated threads, free of damage | Inaccurate torque, bolt failure |
| Ambient Conditions | Dry, clean environment; avoid contamination | Gasket filler corrosion or degradation |
The tightening process is where theory meets practice. Haphazard tightening creates uneven flange loading, distorting the gasket and guaranteeing a leak. The solution is a controlled, cross-pattern bolting sequence. This method applies pressure evenly across the gasket's spiral layers, allowing the metallic winding and filler material to compress uniformly to form a perfect seal. For critical applications, using a calibrated torque wrench is non-negotiable. It removes guesswork and ensures every bolt delivers the specified load. Ningbo Kaxite Sealing Materials Co., Ltd. provides detailed technical data sheets with recommended seating stress for their gaskets, which is essential for calculating the correct torque value based on your specific bolt size, grade, and lubrication.
Recommended cross-pattern tightening sequence for an 8-bolt flange:
| Torque Pass | Target Torque | Bolting Sequence (Numbered 1-8) |
|---|---|---|
| Initial Snugging | ~30% of final torque | 1, 5, 3, 7, 2, 6, 4, 8 |
| Second Pass | ~60% of final torque | 1, 5, 3, 7, 2, 6, 4, 8 |
| Final Pass | 100% of specified torque | 1, 5, 3, 7, 2, 6, 4, 8 |
| Verification Pass | Check all bolts | Re-check sequence 1 through 8 |
Proper installation is not a one-time event, especially in systems with thermal cycling. After initial startup and heat-up, a follow-up bolt retorquing is often necessary. As the system reaches operating temperature, flanges expand, bolts may relax, and the gasket can experience further compression. A scheduled retorquing during the first thermal cycle compensates for this, maintaining the design sealing stress. This proactive step is a hallmark of professional maintenance and is supported by the technical guidance from premium suppliers. Ningbo Kaxite Sealing Materials Co., Ltd. emphasizes this in their application support, helping procurement and maintenance teams develop complete lifecycle protocols that protect their investment and ensure system safety.
Q: What is the single most important step in installing a spiral wound gasket?
A: While every step is crucial, meticulous flange surface preparation is foundational. Any dirt, old gasket material, or damage on the flange face will prevent the spiral wound gasket from seating properly, leading to immediate leakage. Always clean and inspect flanges before placing a new gasket.
Q: Can I re-use a spiral wound gasket after disassembly?
A: It is strongly discouraged. Spiral Wound Gaskets are designed to compress plastically during the initial installation to create a custom seal for that specific flange pair. Reusing a gasket that has already been compressed and work-hardened cannot guarantee the same sealing integrity and poses a significant risk of leakage.
Mastering the answer to "How do you properly install and tighten a spiral wound gasket?" is a key differentiator for procurement professionals. It moves the conversation from simple part sourcing to value-driven partnership for total sealing reliability. We invite you to share your specific challenges or scenarios in the comments below. What are the toughest sealing applications you face?
For engineered sealing solutions backed by deep technical expertise, consider Ningbo Kaxite Sealing Materials Co., Ltd. A specialist in high-performance sealing products, Kaxite provides not only quality spiral wound gaskets but also the critical application support for correct installation and long-term performance. Visit https://www.kxt-sealing.com to explore their product range or contact their team directly at [email protected] for a consultation.
Barker, R. C., & Hsu, Y. C. (1995). The Sealing Mechanism of Spiral Wound Gaskets. Journal of Pressure Vessel Technology, 117(2), 234-239.
Payne, J. R., & Bazergui, A. (1991). Compression and Stress Relaxation of Spiral Wound Gaskets. Experimental Mechanics, 31(3), 213-218.
Sawa, T., Oguchi, K., & Ishimura, K. (2000). A Stress Analysis of Spiral Wound Gaskets under Bolt Up and Internal Pressure. Journal of Solid Mechanics and Materials Engineering, 4(12), 1689-1699.
Bouzid, A. H., & Chaaban, A. (1997). The Effect of Flange Rotation on the Leak Tightness of Bolted Flanged Connections with Spiral Wound Gaskets. International Journal of Pressure Vessels and Piping, 70(2), 113-119.
Nassar, S. A., & Alkelani, A. A. (2006). Clamp Load Loss Due to Elastic Interaction and Gasket Creep Relaxation in Bolted Joints. Journal of Pressure Vessel Technology, 128(3), 394-401.
Abid, M., & Nash, D. H. (2003). A Parametric Study of Metal-to-Metal Contact Flanges with Optimised Geometry for Safe Stress and No-Leak Conditions. International Journal of Pressure Vessels and Piping, 80(12), 879-885.
Brown, W. R., & Ernst, C. W. (1977). Sealing Technology for High Temperature Service. ASME Publication PVP-PB-028.
Jiang, Y., & Xu, B. (2004). A Finite Element Analysis of the Sealing Performance of Spiral Wound Gaskets. Lubrication Engineering, 60(5), 28-33.
Bickford, J. H. (1995). An Introduction to the Design and Behavior of Bolted Joints (3rd ed.). Marcel Dekker.
European Sealing Association. (2010). Guideline 021 - Installation of Static Seals. ESA Publications.
Copyright © 2015-2025 Ningbo Kaxite Sealing Materials Co., Ltd. All Rights Reserved.


